Views: 0 Author: Site Editor Publish Time: 2026-09-16 Origin: Site


Starting a production run without a strict checklist is a massive risk. We frame the pre-run checklist not just as an operational necessity, but as a critical risk-management tool. In high-volume gravure printing, a single setup oversight quickly ruins resources. It can result in thousands of meters of wasted substrate. It also causes costly machine downtime.
You need a reliable system. A successful pre-run protocol relies on standardized, repeatable checks. These checks must cover mechanical integrity, material readiness, system calibration, and safety compliance. Missing even one step compromises the entire job. Precision matters before the cylinders even begin turning.
This guide applies directly to modern production environments. It covers everything from standard web presses to highly advanced electronic drive systems. By following these structured guidelines, you protect your equipment and ensure top-tier print quality. You will learn exactly how to validate your setup, calibrate your tension zones, and eliminate startup defects before they multiply.
Mechanical validation of the engraved cylinder and doctor blade prevents irreversible damage to the printing unit.
Precise ink viscosity management and substrate alignment are mandatory for maintaining color consistency, especially on non-porous films.
Advanced drive systems (like electronic shafts) require specific pre-registration digital checks compared to traditional mechanical line shafts.
Strict adherence to safety and environmental checks (ventilation, static elimination) mitigates the high risks associated with solvent-based inks.
Mechanical components endure extreme stress during high-speed printing. Failing to inspect these parts leads directly to print defects and equipment degradation. You must systematically verify the condition of your cylinders, doctor blades, and impression rollers.
The engraved cylinder serves as the heart of your printing unit. Any surface flaw transfers directly to your substrate. Operators must follow a strict inspection protocol before installing the cylinder into the press.
Visual Cleaning: Wipe the cylinder using an approved solvent. Remove all protective oil applied during storage.
Defect Scanning: Inspect the surface under bright, angled lighting. Look for fine scratches, residual dried ink, or chrome wear. Scratches often cause continuous lines on the printed web.
Cell Inspection: Use a magnification loupe. Ensure the engraved cells remain free of dried ink particles. Plugged cells cause missing dots and poor color density.
Journal Check: Examine the cylinder journals. Ensure they show no signs of excessive wear. Worn journals cause cylinder bounce at high speeds.
The doctor blade wipes excess ink from the non-image areas of the cylinder. Incorrect blade setup remains a leading cause of print failure. You must verify both the angle and the applied pressure.
Set the blade angle typically between 45° and 60°. The exact angle depends on your specific application and cell geometry. You must check for uniform pressure across the entire cylinder width. If the pressure varies, ink film thickness will fluctuate.
Improper blade oscillation or excessive pressure creates severe risks. Heavy pressure leads to accelerated cylinder wear. It destroys the protective chrome layer rapidly. Furthermore, a non-oscillating blade traps metallic debris. This trapped debris scores the cylinder, causing permanent damage. Always confirm the oscillation motor engages properly before circulating ink.
The rubber impression roller forces the substrate into the engraved cells. Capillary action then transfers the ink. This process demands perfectly even pressure.
Inspect the rubber surface closely. Ensure the rubber remains completely clean. Hardened ink on the roller creates localized pressure spikes. Look out for flat spots. Flat spots develop when operators leave the roller engaged during prolonged machine stops. Finally, align the roller to apply even pressure across the entire web width. Uneven alignment causes the web to drift and wrinkle.
Preparing your materials requires exact precision. If the substrate path or ink chemistry fails, mechanical perfection cannot save the print job. You must validate both systems thoroughly.
Threading a complex press correctly takes concentration. Confirm the correct web path according to the specific job schematic. A single missed idler roller alters web tension drastically.
Different materials demand different handling. When operating a film gravure printing machine, you must pay special attention to surface energy. Verify the corona treater is active if the job requires it. Low-surface-energy plastics like BOPP or PE resist liquid. The corona treater oxidizes the film surface. This essential step ensures proper ink adhesion. Without it, the ink easily flakes off the dried plastic.
Ink viscosity dictates color consistency. As solvent evaporates during the run, viscosity increases. You must establish a precise baseline before circulation begins.
Measure baseline ink viscosity using standard efflux cups. A Zahn #2 cup remains the industry standard for this task. Dip the cup, lift it, and time the flow. Compare this baseline against your job ticket specifications.
You must also confirm the solvent blend. The blend must suit the current ambient temperature and humidity. Fast-drying solvents work well in winter. In summer, they evaporate too quickly. Rapid evaporation causes ink drying on the cylinder. This leads to a defect called screening. Conversely, excessively slow solvents cause poor transfer and blocking in the rewind roll.
Parameter | Standard Target | Quality Risk if Ignored |
|---|---|---|
Zahn Cup #2 Viscosity | 18 - 25 seconds | Color shifts, dot gain, screening |
Doctor Blade Angle | 45° - 60° | Scumming, cylinder wear, streaking |
Impression Hardness | 65 - 80 Shore A | Poor ink transfer, web wrinkling |
Corona Treatment | 38 - 42 Dynes/cm | Total loss of ink adhesion on films |
Your ink delivery system requires unobstructed flow. Ensure ink pumps function smoothly without surging. Surging pumps create inconsistent ink levels in the pan.
Inline magnetic filters demand your attention. Keep them clear. These filters catch microscopic metallic debris generated by blade friction. If metallic debris bypasses the filter, it reaches the doctor blade. It will then lodge beneath the blade and gouge the cylinder surface.
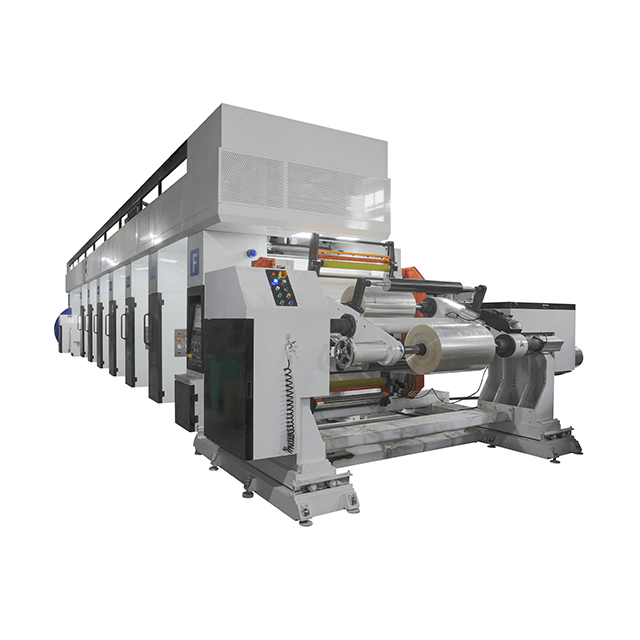
High-speed printing stretches and manipulates the substrate. Proper tension and registration calibration keep the colors aligned perfectly. You must configure these settings digitally and mechanically before hitting the start button.
A modern press divides tension into multiple zones. You must check tension settings at the unwind, infeed, printing units, outfeed, and rewind stations. Each zone requires specific parameters.
Do not assume standard tension works for all materials. This remains a common and expensive mistake. Paper tolerates high, rigid tension. Extensible films behave differently. Films stretch under load. They require distinct taper tension profiles compared to paper. Taper tension gradually decreases the winding force as the roll diameter grows. This prevents the inner layers of the finished roll from telescoping or crushing under extreme pressure.
Color registration relies on exact cylinder alignment. Setting this up efficiently saves immense amounts of substrate.
Complex configurations require careful handling. When preparing an 8 color gravure printing machine, you must align the pre-registration marks carefully. Physically and digitally align these marks on all eight cylinders before you engage the web. This crucial step minimizes setup waste. If you skip pre-registration, the press will waste hundreds of meters hunting for the correct color alignment.
Modern presses handle this differently than older models. If utilizing an electronic shaft rotogravure printing machine, your workflow changes. You must verify servo motor synchronization and zero-reference points directly via the HMI (Human-Machine Interface). You no longer need to check mechanical gearboxes, line shafts, or compensator rollers. The electronic shaft handles phase adjustments digitally. Confirm the network communication shows no faults before proceeding.
Gravure printing often involves highly volatile solvents. Safety checks are never optional. They protect your facility from catastrophic fires and keep operators safe from toxic exposure.
Solvent evaporation generates massive amounts of fumes. Confirm drying hoods are properly sealed. A leaking hood allows toxic vapor to escape into the production hall.
You must verify the Lower Explosive Limit (LEL) sensors. Ensure these sensors remain calibrated and active. Solvent vapors become highly explosive at specific concentrations. The LEL system constantly monitors the air inside the drying exhaust. If vapor concentrations approach dangerous levels, the system increases exhaust fan speed or shuts down the press. This constitutes a non-negotiable compliance check for all solvent-based operations.
Static electricity acts as a hidden enemy in printing facilities. You must ensure anti-static bars or passive static brushes are grounded properly. Test them to confirm they function.
High-speed friction on plastic films creates significant static charges. Unwinding and rewinding plastic webs act like giant static generators. In solvent environments, a single static spark easily serves as an ignition source. Discharging this static before it enters the inking units prevents flash fires. Keep anti-static pins clean; ink buildup ruins their effectiveness.
Machine safety hardware requires physical validation. Do not assume E-stops work simply because they look intact.
Physically test localized E-stops around the press. Press them and confirm they sever power to the drives immediately. Furthermore, confirm machine guards and interlocks are fully engaged. Interlocks prevent the press from running if a guard door remains open. Defeating these interlocks violates safety protocols and endangers the crew.
You have inspected the mechanics, calibrated the tension, and verified safety. Now, you must prove the setup works. The pre-run proof catches subtle errors before you ramp up to production speeds.
Never accelerate a press immediately after setup. Engage the impression rollers at a crawl speed. This slow motion allows you to observe the machine behavior safely.
Verify the ink transfer visually. Ensure the web tracking remains stable through the drying tunnels. Watch the rewind station carefully. The roll should build evenly without telescoping or starring. If the web wanders at crawl speed, it will snap at full speed. Correct any alignment issues immediately.
Quality assurance requires objective measurement. Pull a physical proof from the delivery end of the press. Examine it under a standardized viewing booth (typically D50 lighting).
Check for Drag-Outs: Look for ink smearing past the intended image area, indicating blade issues.
Spot Missing Dots: Inspect highlights and midtones to ensure complete ink transfer from the cells.
Identify Scumming: Watch for a hazy background tint, which suggests the doctor blade isn't wiping the cylinder clean.
Do not rely solely on human eyes for color accuracy. Measure primary color blocks against the approved client proof using a spectrophotometer. Perform a Delta E verification. Delta E calculates the exact numerical distance between the target color and the printed color. Most high-end brands require a Delta E of less than 2.0. If your readings exceed this, you must adjust your ink formulation before proceeding.
Establish a binary decision framework for your operators. This Go/No-Go logic removes emotion and guesswork from the startup process.
Base your final decision on three strict pillars: print quality, tension stability, and drying efficiency. Does the color match the target? Does the web hold perfect tension without wrinkling? Are the LEL sensors reporting safe exhaust levels? If you answer yes to all three, you have clearance. You can confidently ramp up the press to full production speed, often exceeding 300 meters per minute.
A rigorous, documented pre-run checklist directly impacts your bottom line. It serves as your primary defense against catastrophic waste. By standardizing your cylinder inspections, tension calibrations, and safety protocols, you drastically reduce setup waste. This disciplined approach leads to an immediate improvement in Overall Equipment Effectiveness (OEE).
We advise decision-makers to audit their current Standard Operating Procedures against this checklist. Identify the gaps in your current workflow. Train your operators to follow these steps strictly for every single run.
Finally, if your setup times remain unprofitably long despite best efforts, you must evaluate your hardware. It may be time for equipment upgrades. Retrofitting automated viscosity controllers eliminates manual Zahn cup errors. Migrating to a fully motorized or electronic shaft gravure printing machine slashes registration times. Upgrading your technology ensures you remain competitive, profitable, and safe in modern packaging markets.
A: Replacement frequency depends on predictive maintenance rather than a strict timeline. Base your decision on run length, cylinder abrasiveness, and print quality degradation. Abrasive inks like white titanium dioxide wear blades faster. Replace the blade immediately if you notice scumming, streaking, or if the blade edge shows visible micro-fractures during inspection.
A: Web tension loss at startup usually points to pneumatic brake calibration issues at the unwind station. It can also stem from incorrect tension setpoints in the HMI for your specific substrate. Ensure you have programmed the correct taper tension profile. Extensible films require different handling than rigid paper or foil webs.
A: The ideal starting range typically sits between 18 and 25 seconds when measured using a Zahn #2 cup. However, this varies significantly based on ink chemistry, solvent blends, and targeted machine speed. Always match the viscosity to the specific job ticket requirements and maintain it using automated controllers during the run.